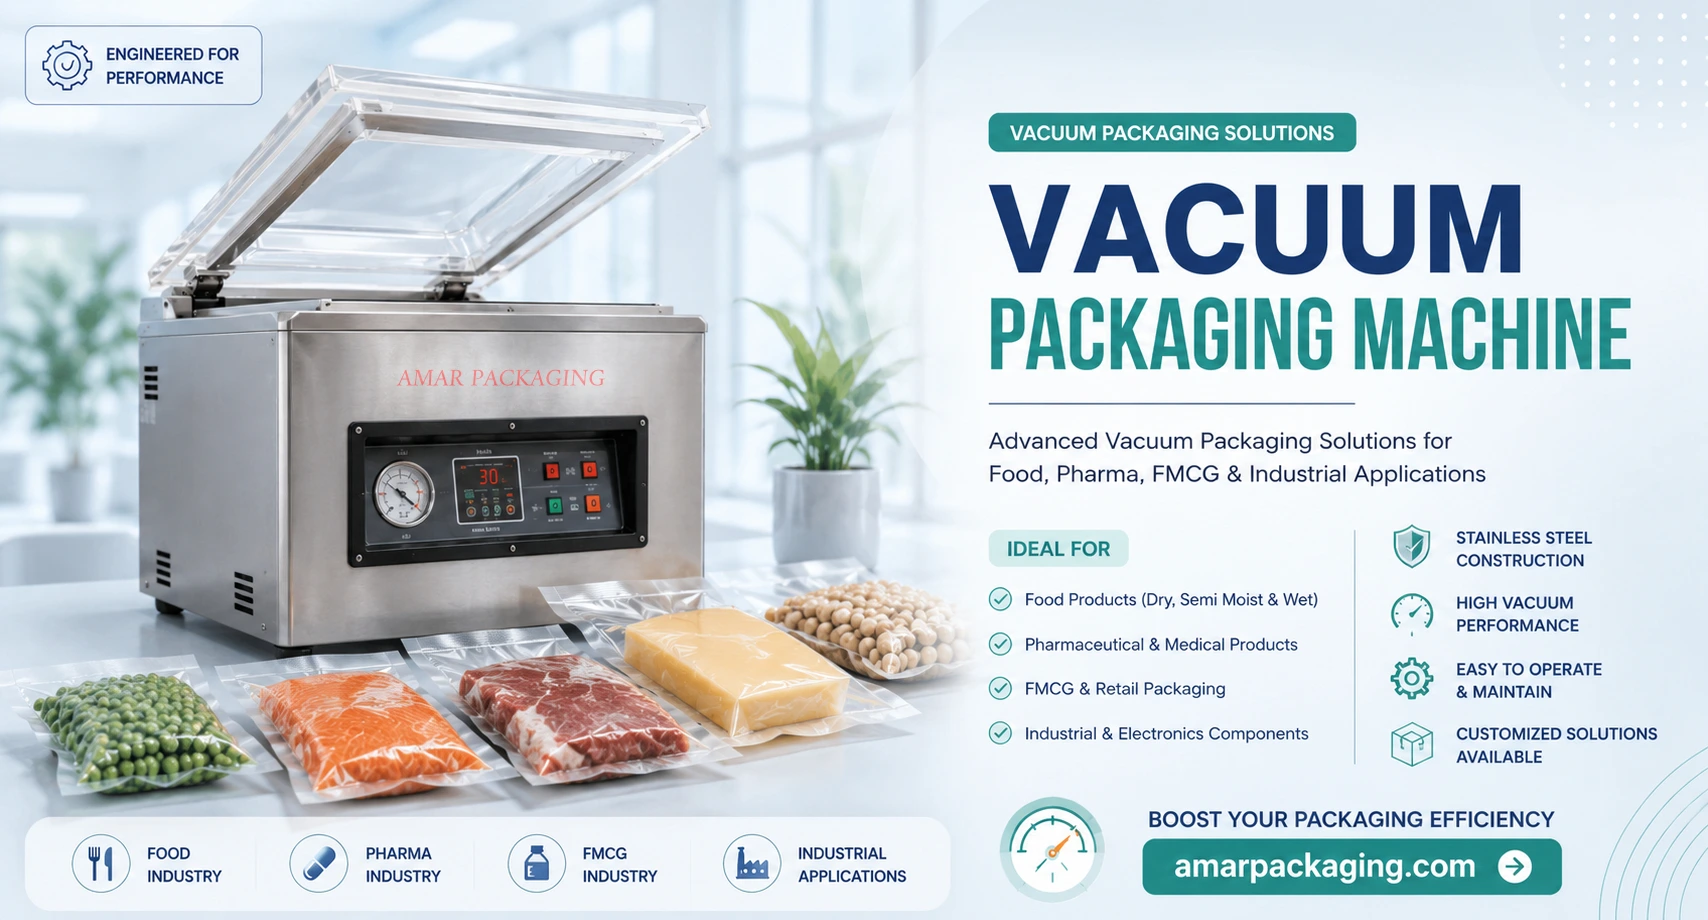
A tabletop vacuum packaging machine is the most direct way an Indian food, pharma or FMCG unit can extend shelf life, cut spoilage and present a cleaner pack — without committing to a full floor-standing line. In a single cycle it pulls air out of a pouch, seals it tight, and hands you a pack that resists oxidation, moisture and pests. This guide explains how the machine works, where it fits across industries, the specifications that actually matter, and how to choose the right unit for your production.
Air is the enemy of almost everything you pack. Oxygen oxidises fats and turns snacks rancid, feeds mould on bread and cheese, and lets aerobic bacteria multiply on meat and fish. Moisture cakes spices and softens biscuits. For decades the standard fix in Indian kitchens and small factories was an impulse sealer and a hope. A vacuum machine replaces that hope with a controlled process — and a compact tabletop unit puts that process within reach of even a single-operator FSSAI business.
Here’s the whole thing in four beats. Once your operator dials in the right settings for a pouch, the digital panel remembers them — so pack number one and pack number one thousand come out identical.
Cycle
One vacuum cycle, four steps
1
Place
Open end of the filled pouch sits over the seal bar.
2
Vacuum
Lid closes; the pump pulls air from the whole chamber.
3
Seal
The heated bar welds the pouch at your set time.
4
Release
Chamber re-pressurises; lift out a tight vacuum pack.
How the vacuum packaging machine builds a stronger seal
The quality of a vacuum pack comes down to three controllable variables: vacuum level, seal time and seal-bar temperature. The vacuum level — how much air is removed, shown on the gauge in mbar — determines how tightly the film clings to the product and how little oxygen is left behind. Seal time and temperature decide how strongly the two layers of film are welded together.
For wet products like marinated meat or fish, the machine offers a soft-air or vacuum-stop adjustment. This seals the pouch at the point where the contents start to bubble, before liquid is drawn out into the chamber — a small control that separates a professional machine from a consumer sealer. Add an optional gas-flush (nitrogen) line and the same machine can replace the evacuated air with an inert gas, which is how snack and dry-food packers keep chips crisp and cushioned without crushing them.
Key applications across food, pharma and FMCG
The reason a single tabletop machine earns its place on so many shop floors is its range., Below are the four industry buckets Amarpack machines most commonly serve.
Applications
One chamber, four worlds
Food
Meat, fish, paneer, cheese, spices, snacks.
Pharma
Tablets, devices, moisture-sensitive goods.
FMCG
Retail multipacks, sample kits, cosmetics.
Industrial
Spares, fasteners, electronics, rust-prone parts.
The shelf-life difference, made visible
The single biggest reason businesses buy a vacuum machine is shelf life. Removing oxygen slows oxidation and starves the aerobic bacteria and moulds that spoil food. The exact gain depends on the product and on whether packs are chilled, frozen or kept at ambient — but the direction is always the same: vacuum packing buys you significantly more time on the shelf and far less waste in the bin.

Specifications that actually matter
| Specification | What it means | What to look for |
|---|
| Seal bar length | Maximum pouch width you can seal in one go | Match to your largest pouch (e.g. 260–420 mm) |
| Pump capacity | How fast the chamber evacuates air (m³/h) | Higher = faster cycles, deeper vacuum |
| Chamber depth | Height of product the chamber can hold | Enough headroom for bulky or filled packs |
| Cycle time | Seconds per complete vacuum-and-seal | Lower is better for higher daily volume |
| Controls | Vacuum, seal time, soft-air, gas-flush options | Digital, repeatable, with a clear gauge |
A useful discipline: write down the largest pouch you pack and your busiest hour’s volume before you shop. Those two facts decide your seal-bar length and the pump capacity you need — and they prevent the common mistake of buying a machine that is either too small to fit the pouch or too slow for the rush.
Why buy your vacuum machine from Amarpack
Amarpack Machines has built industrial packaging equipment in Mumbai since 1998 — that is 27+ years of focused experience, not a trading desk. Every vacuum packaging machine is manufactured in-house at our Maharashtra facility, which means we build, support and stock spares for exactly what we sell. That in-house manufacturing is the reason our after-sales response and parts availability outperform imported units, and it is why food, pharma and FMCG names across India run Amarpack machines on their lines. Each unit is ISO 9001:2015 and CE compliant, and backed by warranty and engineer support.
💬 Comment “VACUUM” and we’ll send your quote
Find the right machine for your line
Send us your largest pouch size and busiest-hour volume — our engineers will recommend the exact chamber, seal bar and pump, with a clear price in INR.
Request a Quote →
Frequently asked questions
Ready to Upgrade Your Packaging Line Before the Peak Hits?
At Amarpack Machines Private Limited, we’ve helped manufacturers across India find the right shrink tunnel solution for their exact production needs — from compact semi-automatic setups to high-speed fully automatic lines.
📞 Talk to our packaging experts today. We’ll assess your current line, understand your seasonal volumes, and recommend a solution that’s sized right — not just for june, but for every high-demand season ahead.
 Get a Free Consultation → Contact Us
Amarpack Machines Private Limited | Vacuum Packaging Machine| Mumbai, India Trusted by FMCG, Food & Beverage, Pharma, and E-commerce manufacturers across India.