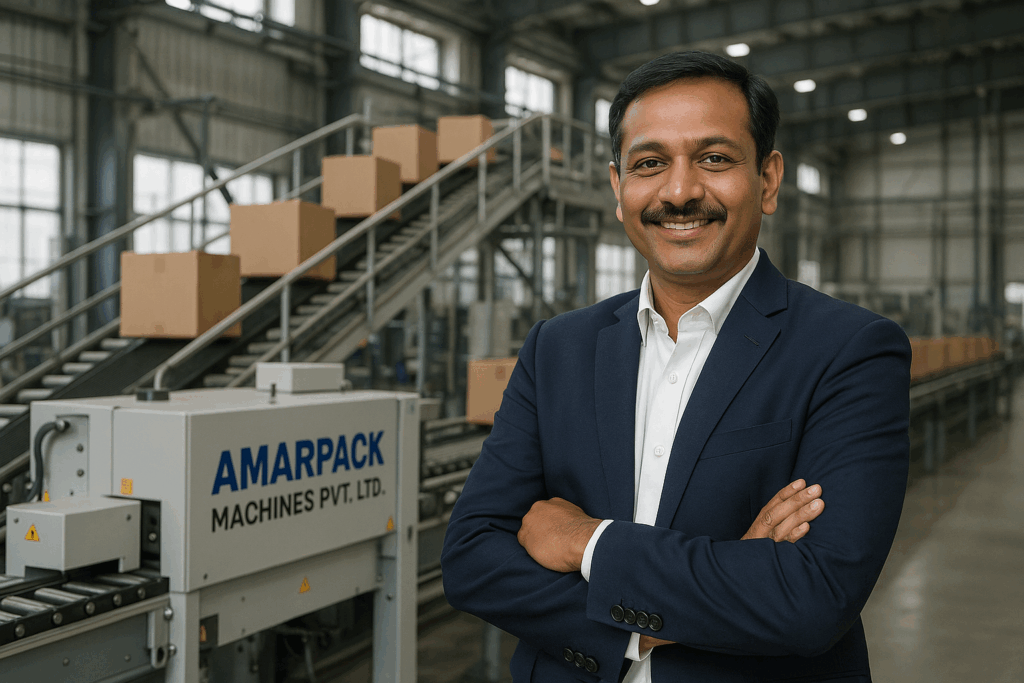
In the fast-paced and precision-driven world of modern manufacturing, conveyor systems play a pivotal role in improving efficiency, reducing labor, and ensuring timely product movement. As the demand for flexible, intelligent, and application-specific automation solutions increases, customized conveyor systems have emerged as a core component of smart manufacturing ecosystems.
From packaging units to assembly lines, customized conveyors are transforming how industries operate by integrating automation, IoT technology, and modular design. This blog explores why investing in a customized conveyor system is not just a good idea—but a strategic move for manufacturers who want to stay competitive in 2025 and beyond.
What Is a Customized Conveyor System?
A customized conveyor system is a material handling solution designed and engineered to meet the specific needs of a manufacturing or packaging process. Unlike standard, off-the-shelf conveyor systems, these are built based on:
- Type of product being handled
- Speed and throughput requirements
- Space constraints
- Industry-specific hygiene or safety standards
- Integration with automation equipment
Whether it’s a modular belt conveyor for packaging, a heavy-duty roller conveyor for industrial components, or a stainless steel food-grade conveyor for the food processing industry, customization enables flawless operations tailored to your unique production goals.
Why Customized Conveyor Systems Are Leading the Future
1. Enhanced Operational Efficiency
Tailor-made conveyor systems are designed to move products with minimal friction, precise alignment, and optimized speed. They significantly reduce manual handling and eliminate bottlenecks. For example:
- Automated conveyor systems integrated with sensors can adjust speeds based on workload.
- Smart conveyors can detect obstructions or damaged goods and reroute the flow.
2. Seamless Integration with Smart Manufacturing Technologies
In 2025, Industry 4.0 is no longer a trend—it’s the standard. Customized conveyors integrate with:
- PLC systems
- IoT devices
- Robotics arms
- Vision inspection systems
- Barcode/RFID scanners
This transforms a basic transport line into an intelligent material flow solution that enables real-time monitoring, predictive maintenance, and adaptive workflow changes.